Coalescing filters remove liquid oil aerosols and water droplets from compressed air and gas streams by merging microscopic droplets into larger ones that gravity and drainage can separate from the flow, while desiccant filters remove water vapor at the molecular level through adsorption onto materials like silica gel or molecular sieve, achieving dew points that coalescing filters cannot reach. Choosing between them depends on whether the contamination problem is liquid-phase oil and moisture or vapor-phase water content that must be dried to a specific dew point.
Key Takeaways
- Coalescing filters capture and merge liquid oil aerosols and water droplets down to 0.01 microns through layered filter media; desiccant filters adsorb water vapor at the molecular level, achieving dew points as low as minus 40 degrees Fahrenheit.
- Coalescing filters are the right choice when the goal is removing liquid-phase oil contamination and bulk moisture from compressed air or gas streams; desiccant filters are the right choice when the goal is drying gas to a precise dew point specification.
- Both coalescing filter housings and desiccant vessel housings operating above 15 psig are pressure vessels under ASME Section VIII Division 1 and require U Stamp certification and hydrostatic testing.
- Many compressed air and natural gas systems use coalescing filters upstream and desiccant filters downstream, with the coalescing stage protecting the desiccant media from liquid loading that would accelerate degradation.
- Desiccant media requires periodic regeneration or replacement; coalescing filter elements require periodic replacement based on pressure drop and contamination load, typically every six to 12 months.
How Coalescing Filtration Works
Coalescing filtration removes liquid contaminants from compressed air and gas streams by capturing fine oil aerosols and water droplets on specialized layered filter media and encouraging those droplets to merge into larger particles heavy enough to drain from the housing under gravity. The process targets liquid-phase contamination, including oil aerosols from compressor carry-over, water droplets from compression and cooling, and fine particulates that travel with the gas stream.
Contaminated gas enters the filter housing and flows through the coalescing media. As the gas passes through, the media captures microscopic droplets as small as 0.01 microns and holds them long enough for coalescence to occur. Merged droplets grow until they become large enough to fall away from the media surface and collect at the bottom of the housing, where a drain system removes them continuously or on a timed cycle without interrupting gas flow.
The result is a cleaner gas stream that protects downstream equipment from oil fouling, corrosion, and contamination. Oil removal efficiency in well-designed coalescing systems reaches 99.9%, making them the standard choice for compressed air systems, fuel gas conditioning packages, natural gas processing, and biogas upgrading applications.
How Desiccant Filtration Works
Desiccant filtration removes water vapor from gas streams through adsorption, a process where water molecules bond to the surface of a solid desiccant material rather than being captured as liquid droplets. Because desiccant filtration targets vapor-phase moisture rather than liquid-phase contamination, it achieves dew points that coalescing filters cannot reach.
Common desiccant materials include silica gel, activated alumina, and molecular sieve, each selected based on the required dew point and the presence of other contaminants in the gas stream. Silica gel handles general moisture removal effectively. Activated alumina performs well in applications with moderate dew point requirements and some hydrocarbon presence. Molecular sieve achieves the deepest dew points, down to minus 40 degrees Fahrenheit or lower, for instrument air, pipeline gas, and specialty gas applications where trace moisture causes operational or product quality problems.
Because desiccant media eventually saturates with adsorbed water, desiccant systems require regeneration or media replacement to restore adsorption capacity. Twin-tower systems address this by alternating between an adsorbing tower and a regenerating tower, delivering continuous dry gas output while each tower cycles through its operating phase.
Coalescing vs Desiccant: Direct Comparison
The table below maps the five most important selection criteria against both filtration technologies. Use it to confirm which technology addresses the specific contamination problem before specifying equipment.
| Criterion | Coalescing Filter | Desiccant Filter |
|---|---|---|
| Mechanism | Captures and merges liquid droplets through layered filter media, then drains them from the housing | Adsorbs water vapor onto desiccant material (silica gel, activated alumina, or molecular sieve) |
| Contaminant Removed | Liquid oil aerosols, water droplets, and fine particulates in the liquid phase | Water vapor and molecular-level moisture in the gas phase |
| Particle or Contaminant Size | Down to 0.01 microns for liquid aerosols | Molecular-level water vapor; achieves dew points to minus 40 degrees Fahrenheit |
| Typical Applications | Compressed air systems, fuel gas conditioning, natural gas processing, biogas upgrading | Instrument air, pipeline gas drying, natural gas transmission, biogas dehydration |
| ASME Applicability | Filter housings above 15 psig require ASME Section VIII U Stamp certification | Desiccant vessel housings above 15 psig require ASME Section VIII U Stamp certification |
As the table shows, the two technologies solve different problems and frequently appear together in the same system. A coalescing filter upstream of a desiccant dryer removes liquid oil and bulk moisture that would otherwise saturate and degrade the desiccant media prematurely, protecting the more expensive desiccant stage while delivering the combined output quality the application requires.
For more on how pressure drop interacts with filter selection and sizing, see understanding pressure drop in coalescing filters. For more on the vessel types used in gas scrubbing and separation applications, see scrubber vessel technology.
Selecting the Right Filtration Technology
Four factors determine whether coalescing filtration, desiccant filtration, or a combination of both is appropriate for a given application.
Contamination type is the primary selection driver. Liquid oil aerosols and bulk water droplets require coalescing filtration. Vapor-phase moisture requiring a specific outlet dew point requires desiccant filtration. Many systems require both because liquid-phase and vapor-phase contamination coexist in the same gas stream.
Required outlet quality sets the performance target. Coalescing filtration achieves residual oil content below 0.01 parts per million and removes bulk moisture as liquid. Desiccant filtration achieves outlet dew points from plus 40 degrees Fahrenheit for basic drying down to minus 40 degrees Fahrenheit or lower for critical applications. The outlet specification drives the technology choice.
Operating pressure and flow rate affect both sizing and ASME code applicability. Filter and desiccant vessel housings operating above 15 psig fall under ASME Section VIII Division 1, requiring U Stamp certification, hydrostatic testing, and Form U-1 documentation. Undersizing filter vessels increases pressure drop and reduces element life. Oversizing increases capital cost without improving performance.
Maintenance access and regeneration requirements affect lifecycle cost. Coalescing elements require periodic replacement based on pressure drop monitoring. Desiccant systems require either twin-tower regeneration cycles or periodic media replacement. Facilities with limited maintenance windows should factor regeneration cycle disruption into the technology selection before committing to a desiccant system configuration.
What Red River Applies
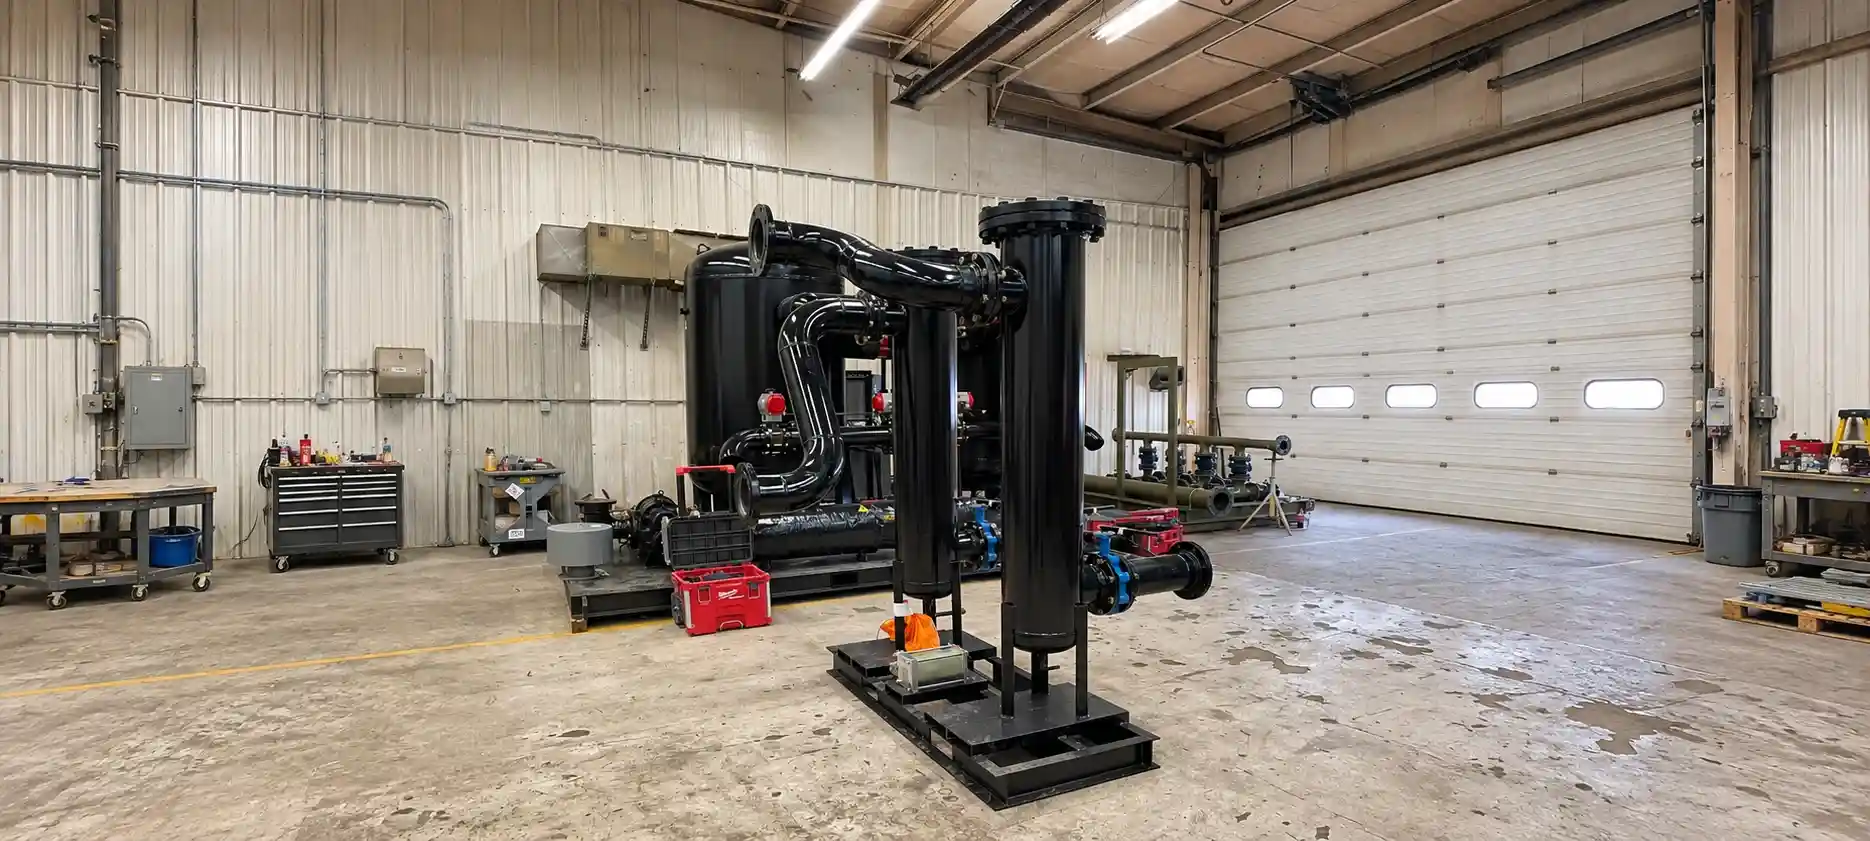
Red River fabricates ASME U Stamp certified pressure vessels including filter housings, scrubber vessels, and coalescing separator vessels for oil and gas, power generation, and biogas applications. Every vessel includes full material traceability, hydrostatic test records, and ASME Authorized Inspector approval before shipment. Modular skid packages integrating coalescing filter housings, inlet separators, and downstream process vessels are engineered and fabricated as complete pre-tested assemblies to the same ASME standards.
For filtration vessel projects, operating pressure, gas composition, flow rate, and outlet quality requirements are reviewed before fabrication begins. The filter housing specification, nozzle sizing, and drain system configuration all depend on the specific contamination load and required outlet quality of the application.
What This Means
Coalescing and desiccant filtration address different contamination problems in compressed air and gas systems. Selecting the wrong technology, or specifying only one when both are needed, results in either ineffective contamination control or premature media degradation that drives up operating costs and reduces system reliability. Understanding the mechanism behind each technology and the contamination type it targets leads to specifications that deliver the required outlet quality from day one rather than requiring field modifications after commissioning.
For procurement managers and engineers evaluating filter vessel specifications, the contamination analysis comes first. The technology selection follows directly from it, and the vessel sizing and ASME code requirements follow from that.
Ready to Discuss Your Filtration Vessel Requirements?
Red River designs and fabricates ASME U Stamp certified filter housings, coalescing separator vessels, and modular skid packages for oil and gas, power generation, and biogas filtration applications. Every build is sized to the system’s operating pressure, flow rate, and outlet quality requirements, and delivered with full ASME documentation. Request a quote or contact the team to discuss your filtration vessel specifications.
Frequently Asked Questions
1. What is the difference between coalescing and desiccant filtration?
Coalescing filtration removes liquid oil aerosols and water droplets from gas streams by capturing them on filter media and draining them from the housing. Desiccant filtration removes water vapor at the molecular level through adsorption onto materials like silica gel or molecular sieve, achieving dew points that coalescing filters cannot reach. The two technologies address different phases of contamination and frequently appear together in the same system.
2. When should a coalescing filter be used instead of a desiccant filter?
Use a coalescing filter when the primary contamination problem is liquid-phase oil aerosols, bulk water droplets, or fine particulates in a compressed air or gas stream. Use a desiccant filter when the application requires a specific outlet dew point specification and the contamination is vapor-phase moisture rather than liquid droplets. Many systems use both in sequence, with the coalescing stage protecting the desiccant media from liquid loading.
3. Do coalescing filter housings and desiccant vessels require ASME certification?
Yes, when operating above 15 psig. Both coalescing filter housings and desiccant vessel housings are pressure vessels under ASME Section VIII Division 1 when they operate above that threshold. They require U Stamp certification, hydrostatic testing at 1.3 times the maximum allowable working pressure, and Form U-1 Manufacturer’s Data Report documentation before entering service.
4. How often do coalescing filter elements need replacement?
Replacement frequency depends on contamination levels and operating conditions, but most coalescing filter elements require inspection every six to 12 months. The best indicator is pressure drop across the filter. As the element loads with oil and particulates, pressure drop increases. Replacement is recommended when pressure drop reaches the manufacturer’s specified limit to maintain flow efficiency and outlet quality.
5. Can coalescing and desiccant filters be used together in the same system?
Yes, and this is the standard configuration for compressed air systems and natural gas processing applications requiring both oil removal and moisture control. The coalescing filter installs upstream to remove liquid oil aerosols and bulk water, then the desiccant dryer removes residual vapor-phase moisture to the required dew point. The coalescing stage protects the desiccant media from liquid loading that would accelerate saturation and reduce drying efficiency.
6. What desiccant materials are used in industrial gas drying applications?
Three desiccant materials cover most industrial applications. Silica gel handles general moisture removal in compressed air systems. Activated alumina performs well where moderate dew points are required and some hydrocarbon presence exists. Molecular sieve achieves the deepest dew points, down to minus 40 degrees Fahrenheit or lower, for instrument air, pipeline gas, and specialty gas applications where trace moisture causes operational or quality problems.