Which Materials Suit Make-Up Water Service?
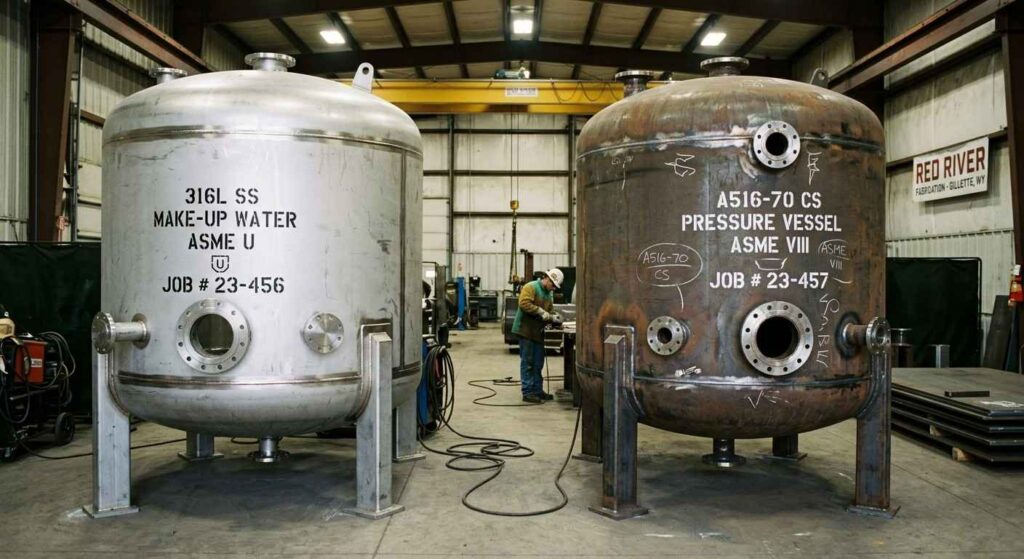
Carbon steel suits most industrial make-up water service when the stored water carries a compatible corrosion inhibitor package, while stainless steel is required where fluid purity matters or where the water chemistry is corrosive to steel. Fiberglass and HDPE serve atmospheric tanks in aggressive chemical service where steel would degrade. Key Takeaways Make up water […]
How Big Should Make-Up Water Tanks Be?
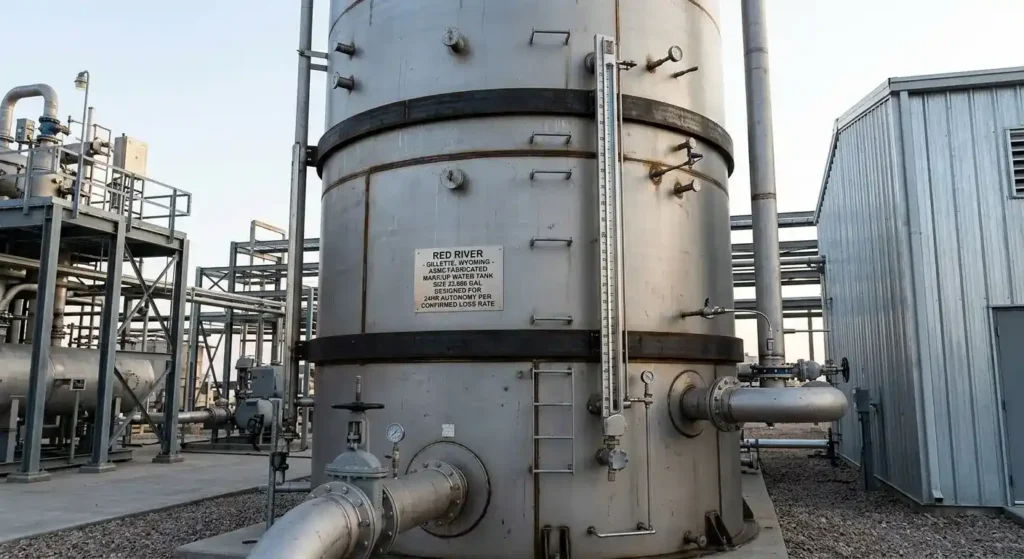
Make-up water tanks should be sized to cover the system’s total daily fluid loss rate multiplied by the required autonomy period in days, plus a reserve margin of 20 to 25 percent above the calculated minimum. The two variables that determine makeup water tank capacity are how fast the system loses fluid and how long […]
When to Spec Equalization Tanks for Industrial Systems
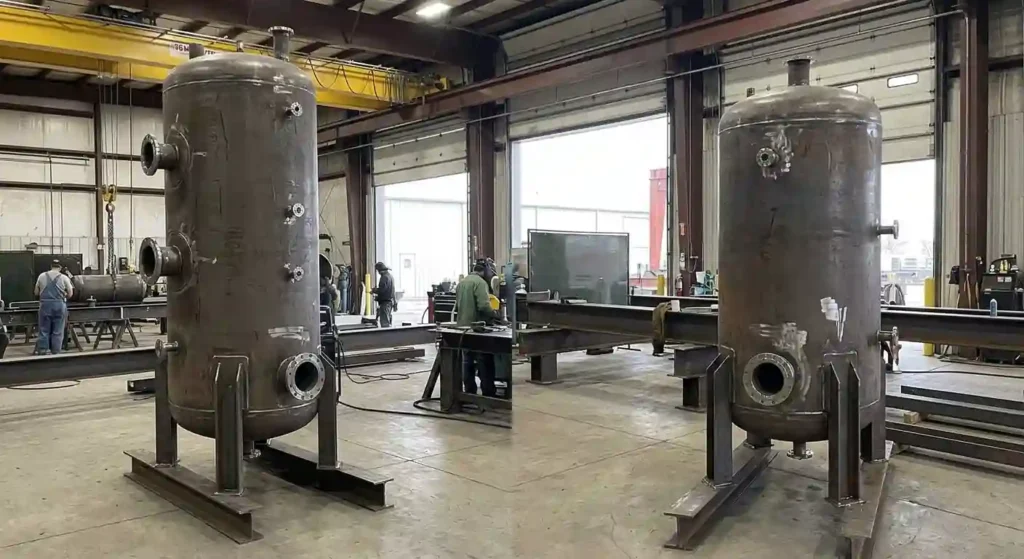
Equalization tanks are required when upstream flow variability exceeds the tolerance of downstream equipment and when concentration, pH, or temperature surges would overload or upset treatment and processing systems. The equalization tank specification trigger is always the gap between what the upstream process produces and what the downstream system was designed to receive. Key Takeaways […]
How Do Equalization Tanks Balance Flow?
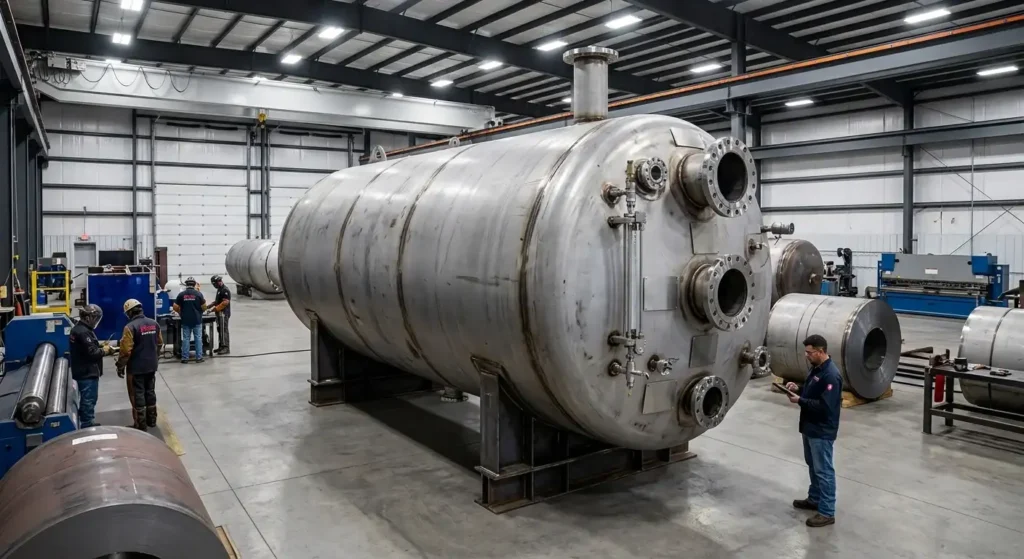
Equalization tanks balance flow by accepting incoming process fluid at variable rates and releasing it at a controlled, steady rate determined by the downstream system’s design capacity. The vessel holds the excess volume that accumulates during peak flow periods and depletes it during low-flow periods, smoothing the hydraulic load seen by downstream treatment or processing […]
What Is an Equalization Tank?
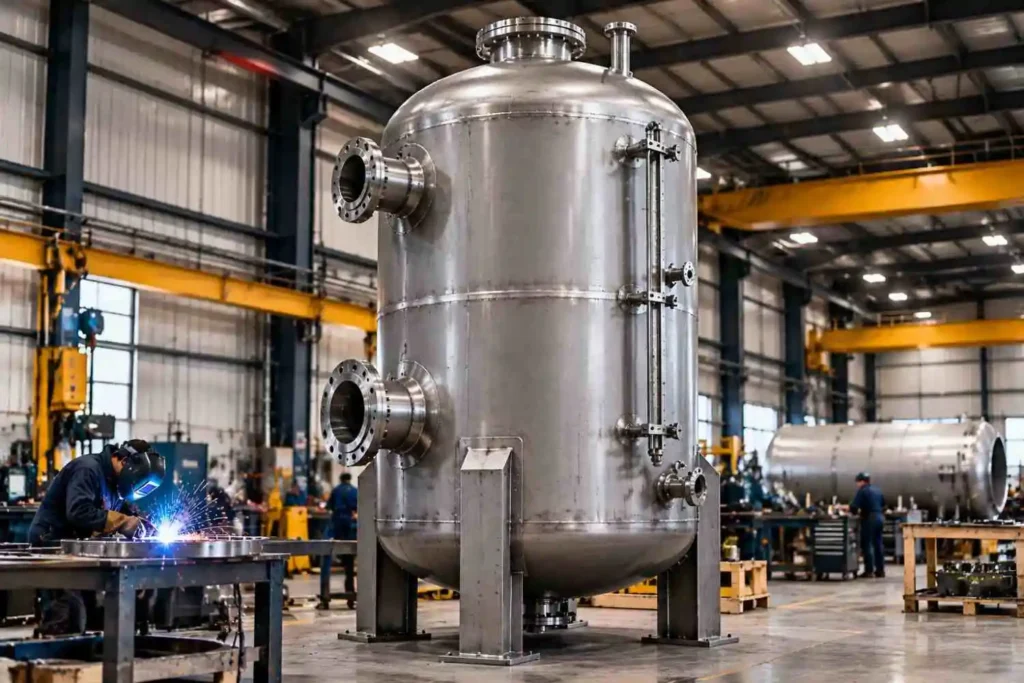
An equalization tank is a holding vessel placed between a variable upstream process stream and a downstream system that requires consistent inlet conditions, buffering fluctuations in flow rate, concentration, pH, or temperature so the downstream equipment receives a steady, controllable feed. Without an equalization tank, surge flows and concentration spikes pass directly into treatment or […]
Which Tests Validate Deaeration in Pressure Systems?
Deaeration is validated through three distinct test types: dissolved oxygen measurement confirms the deaerator achieves the 0.005 cc/liter performance threshold, hydrostatic pressure testing confirms the storage vessel holds pressure to ASME code, and weld NDE confirms the fabrication integrity of every pressure-retaining joint. All three must pass before a deaerator system is considered ready for […]
How to Document NDE Results for ASME Pressure Vessels
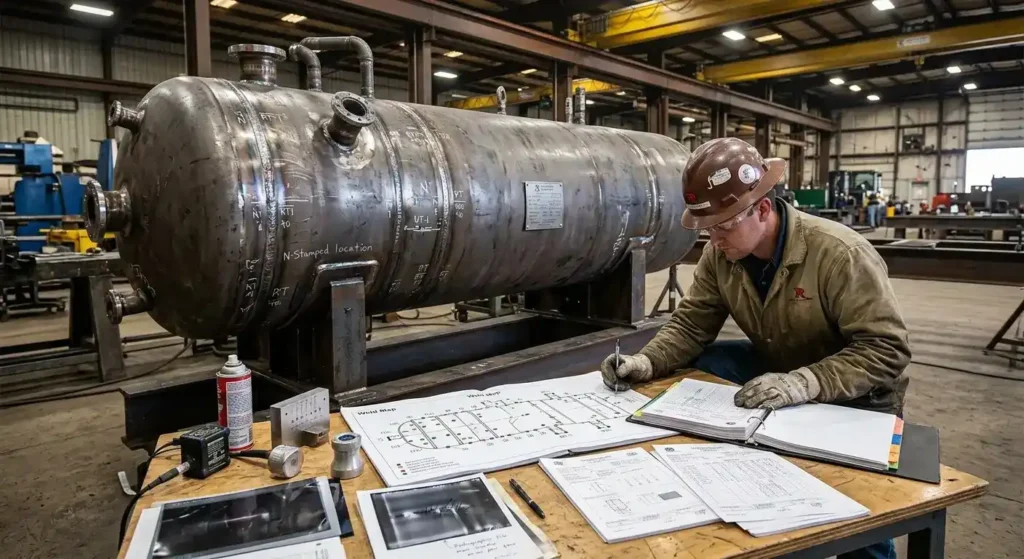
Documenting NDE results correctly comes down to recording six elements for every examination: the weld identity tied to the weld map, the written procedure and revision used, the examiner and their certification level, the raw result and disposition against named acceptance criteria, the formal handling of any reject and re-test, and a dated signature. A […]
When Are Leak Tests Mandated in Pressure Vessel Work?
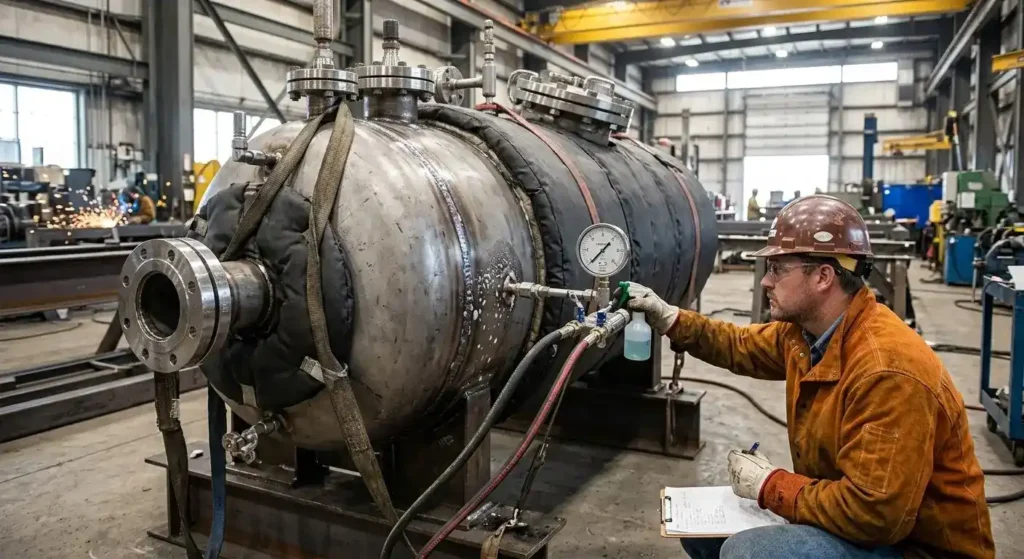
Leak tests are mandated whenever the construction code, the service conditions, or the owner’s specification call for verified leak-tightness, most often for hazardous fluids, vacuum service, certain process piping, and post-repair work. Understanding when leak tests are mandated starts with the governing code and the design basis, not the shop floor. Key Takeaways The construction […]
When Are Deaerators Required in Pressure Systems?
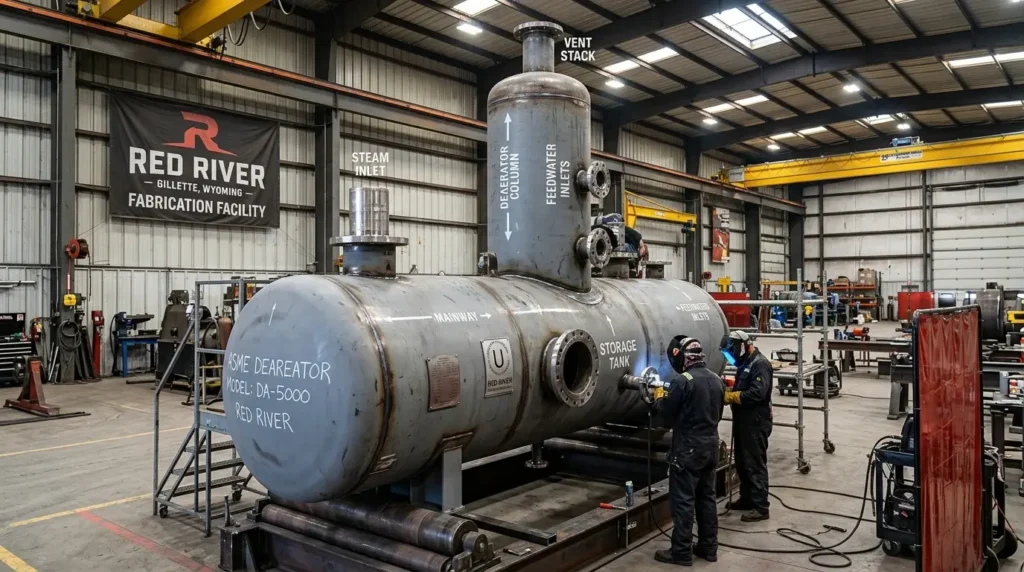
Deaerators are required in steam boiler systems and hot-water heating applications when dissolved oxygen and carbon dioxide must be removed from feedwater to prevent corrosion, pitting, and premature equipment failure. They are mandated by system design standards, boiler codes, and plant operating requirements, and the deaerator pressure vessel must be built to ASME Section VIII […]
How Do Deaerator Tanks Cut Oxygen in Boiler Systems?
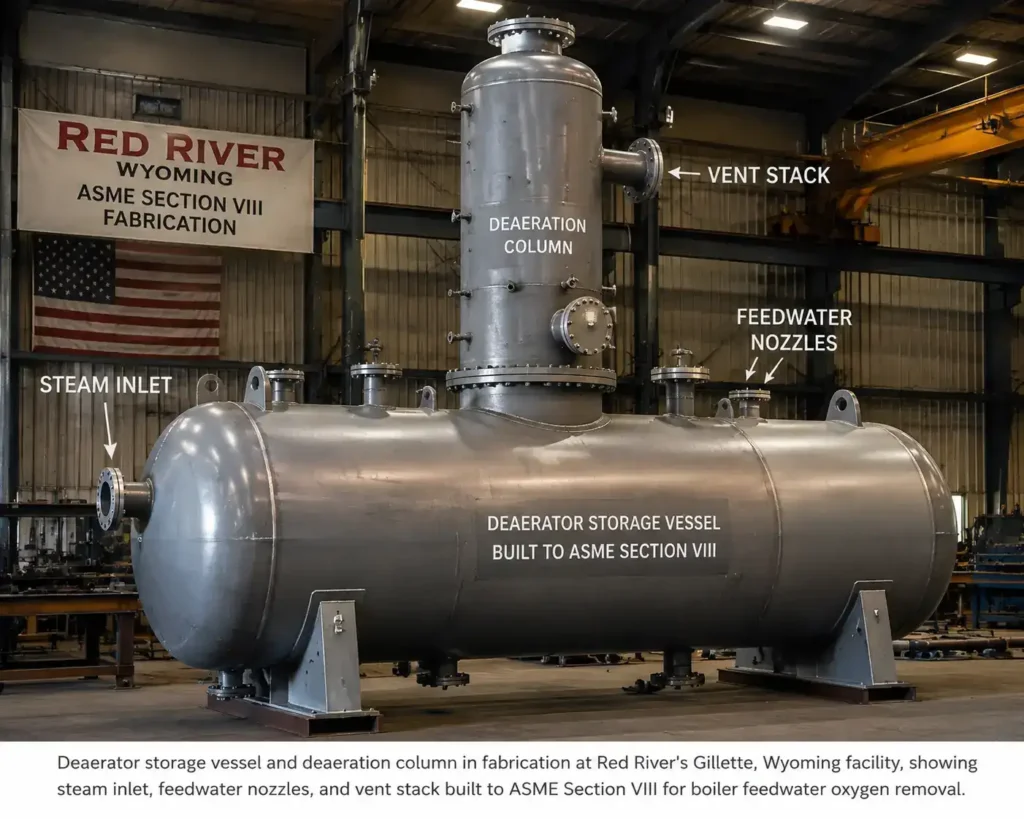
Deaerator tanks cut oxygen by heating boiler feedwater to its saturation temperature and mechanically agitating it so dissolved gases leave solution and vent continuously to the atmosphere, reducing dissolved oxygen to below 0.005 cc per liter. At that level, oxygen pitting corrosion in carbon steel boiler tubes and condensate return lines becomes negligible. Key Takeaways […]